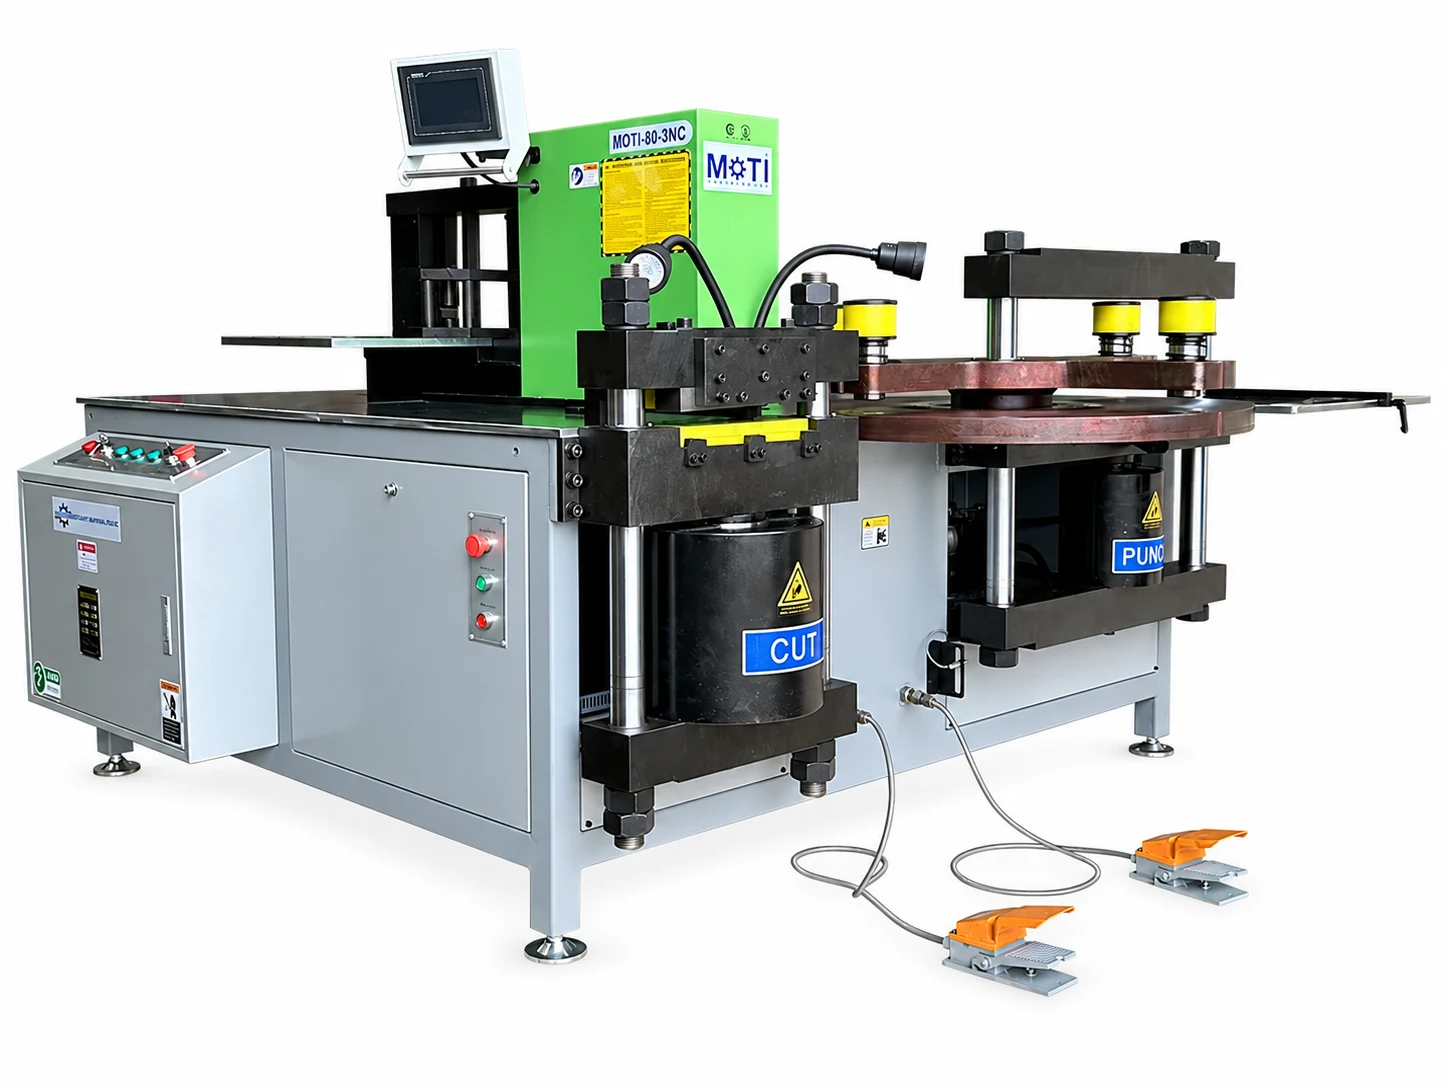
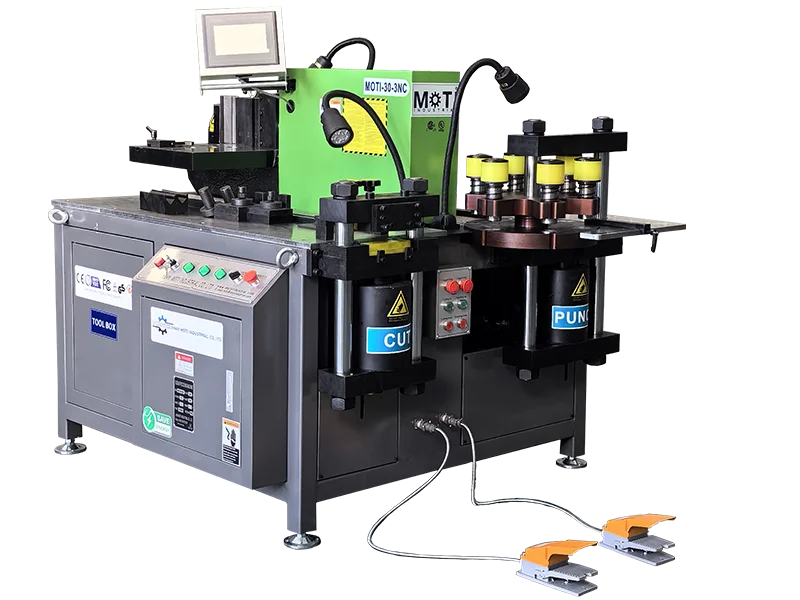
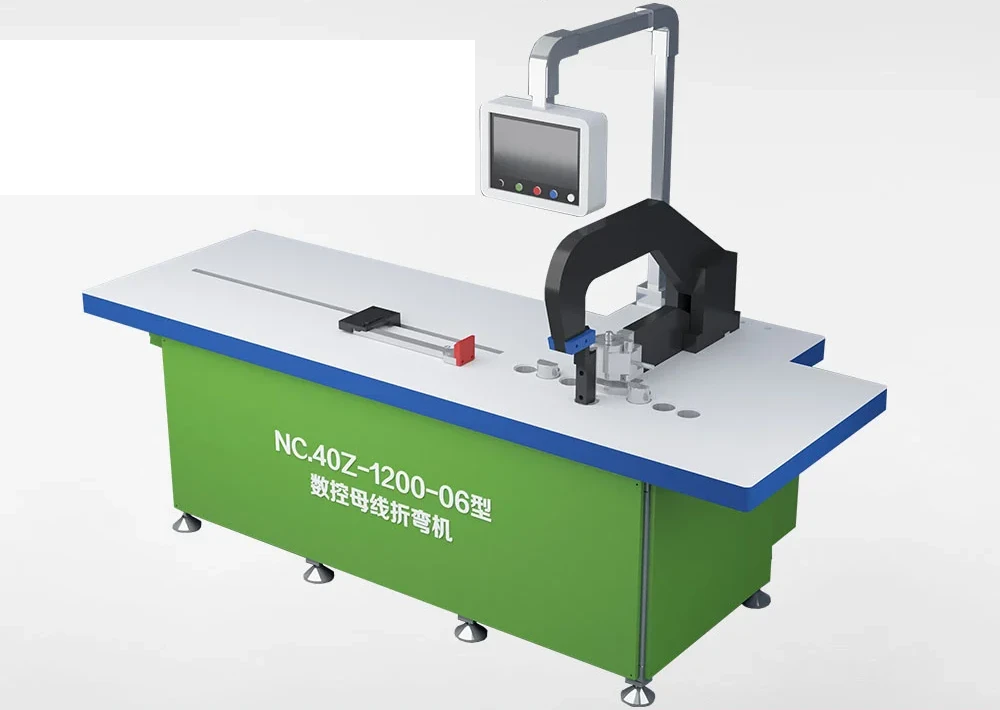
Standard 3-in-1

Cut, punch and bend. Standard, wider MAX and heavy-duty models.

Servo 3-in-1

Four positioning axes. Operators move parts between stations.

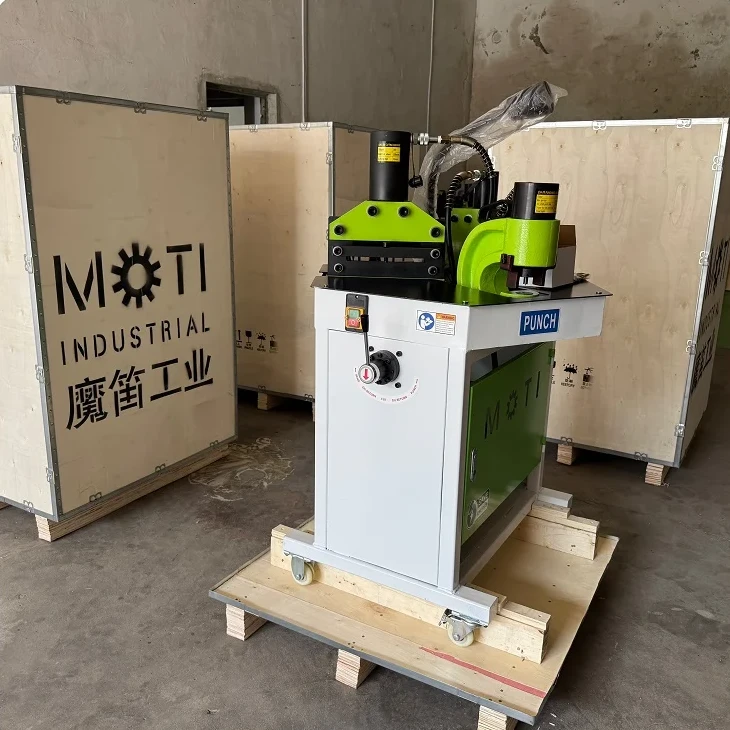
Portable Hydraulic

Separate cutting, punching and bending tools with hydraulic power.

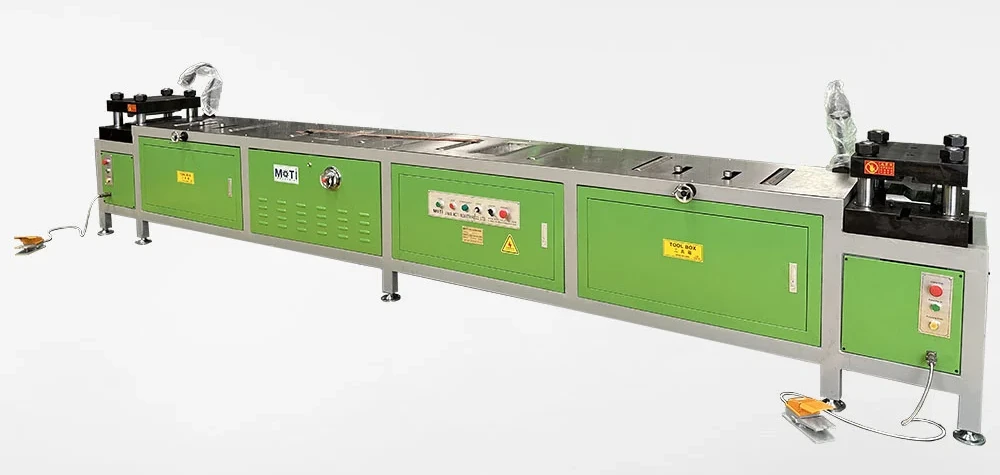
Dedicated Bending

CNC bending centers or double-head busduct connection bending.

3-in-1 workstation

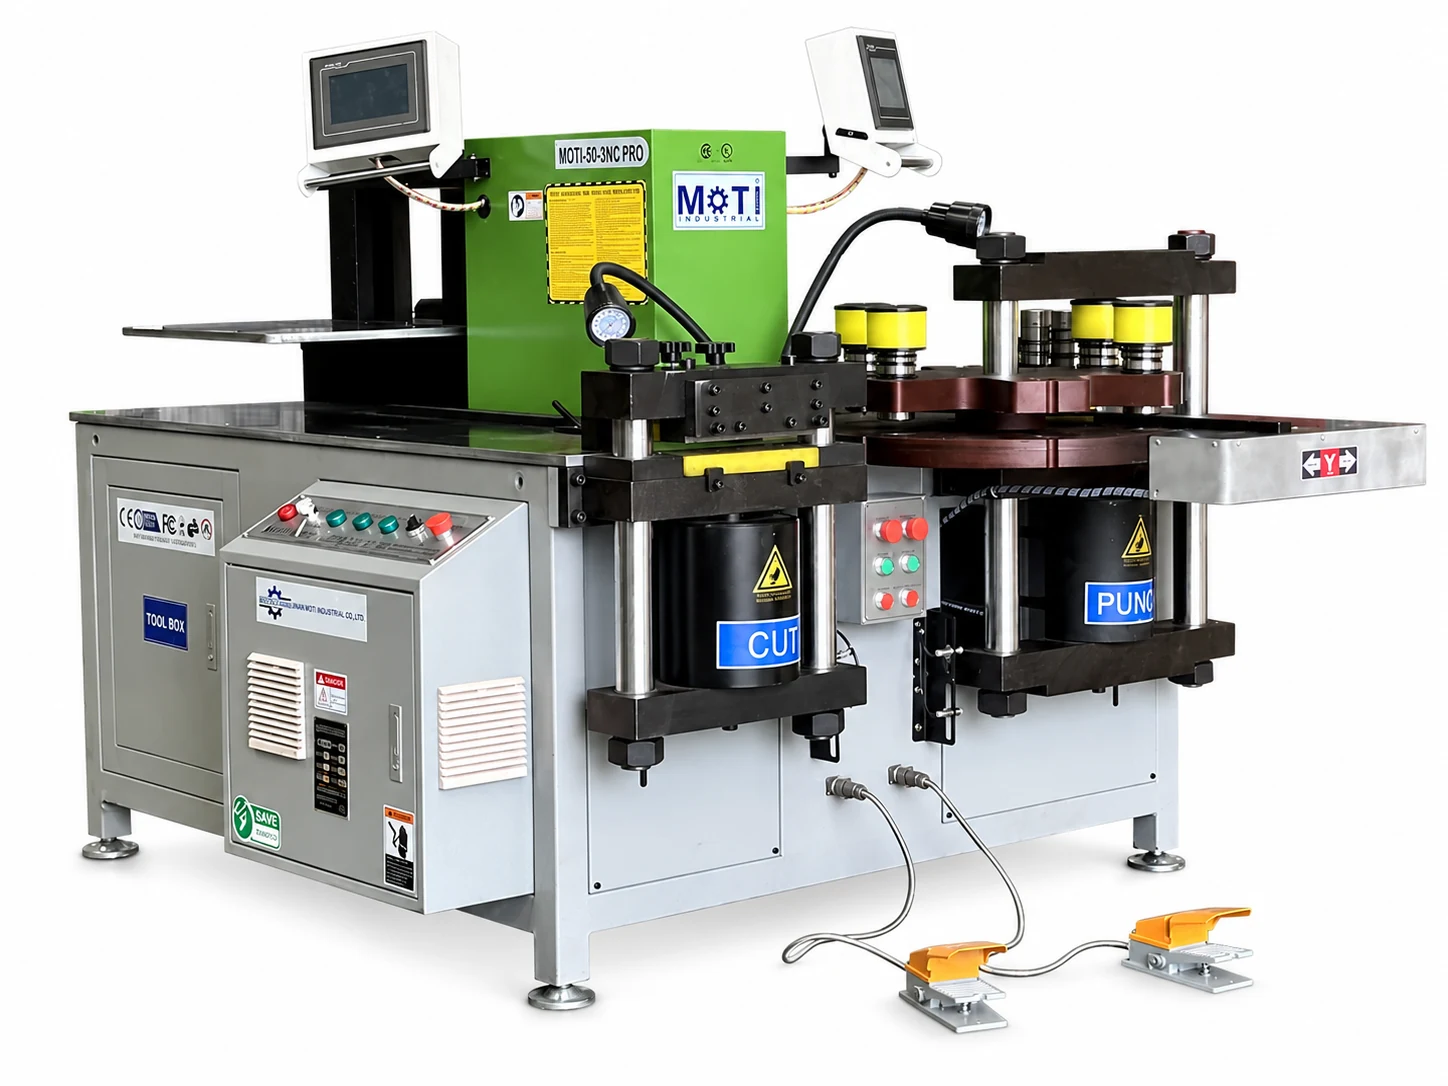
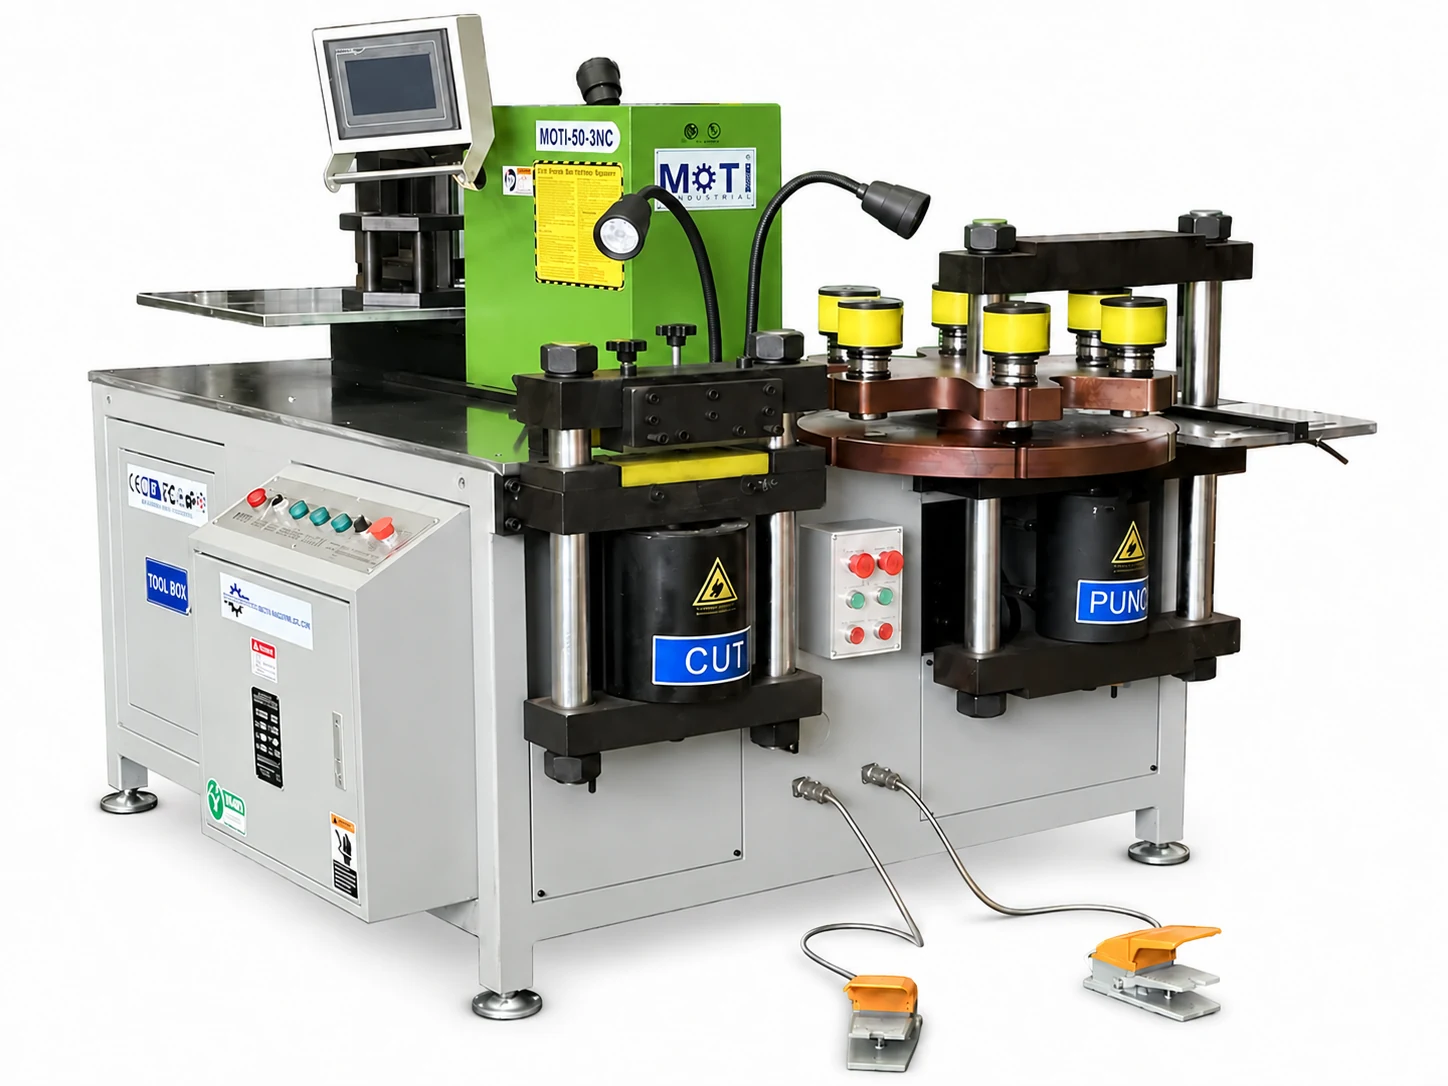
MOTI-50-3NC 3-in-1 Busbar Processing Machine

A wider working range for panel production.

The 50-3NC combines cutting, punching and bending in the 16 mm thickness class. Working width is specified for the selected configuration. Send your connection drawing to review the machine and tooling for your panel designs.

Thickness × width

16 mm thickness; width by configuration

Send your drawing to check material, tooling and operation limits.

THE RIGHT APPLICATION

A larger working range for panel builders with mixed busbar sizes.

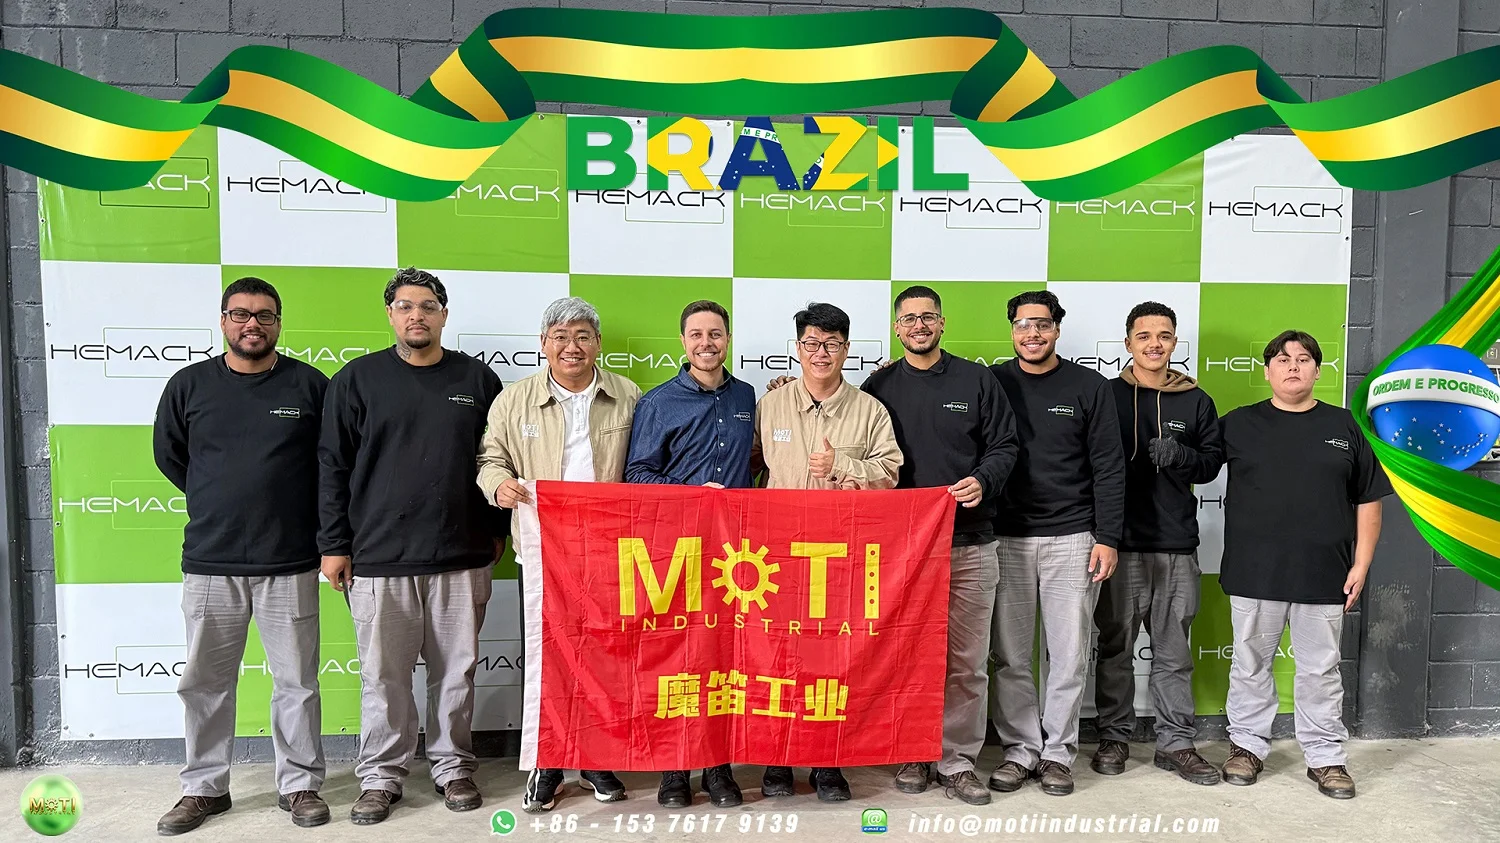
The MOTI-50-3NC brings three independently powered workstations to larger copper connections. It covers the 16 mm thickness class, with working width defined for the selected configuration. For panel builders, compare the actual connection: its hole pattern, bend direction and assembly clearance. Our HEMACK project shows how machine selection can extend to dedicated connection tooling.

01 TECHNICAL OVERVIEW

Know the working range.

Compare these working limits with your part. Your quotation identifies the supplied machine version and tooling.

Machine specifications
Cutting capacity (thickness × width)16 mm thickness; width by configuration
Punching capacity (thickness × width)16 mm thickness; width by configuration
Main bending capacity (thickness × width)16 mm thickness; width by configuration
Punching force500 kN
Bending force500 kN
Machine weight1750 kg
Bending accuracy±1 °
Repeat bending accuracy±0.3 °
Punching diameter4.3–34 mm
Main motors3 × 5.5 kW
Edge bending (width × thickness)120 × 12 mm

Before you choose

Cutting, punching and main bending support the 16 mm thickness class. Working width is specified for the selected configuration. Edge bending has a separate 12 × 120 mm limit.

A clear view of the working units

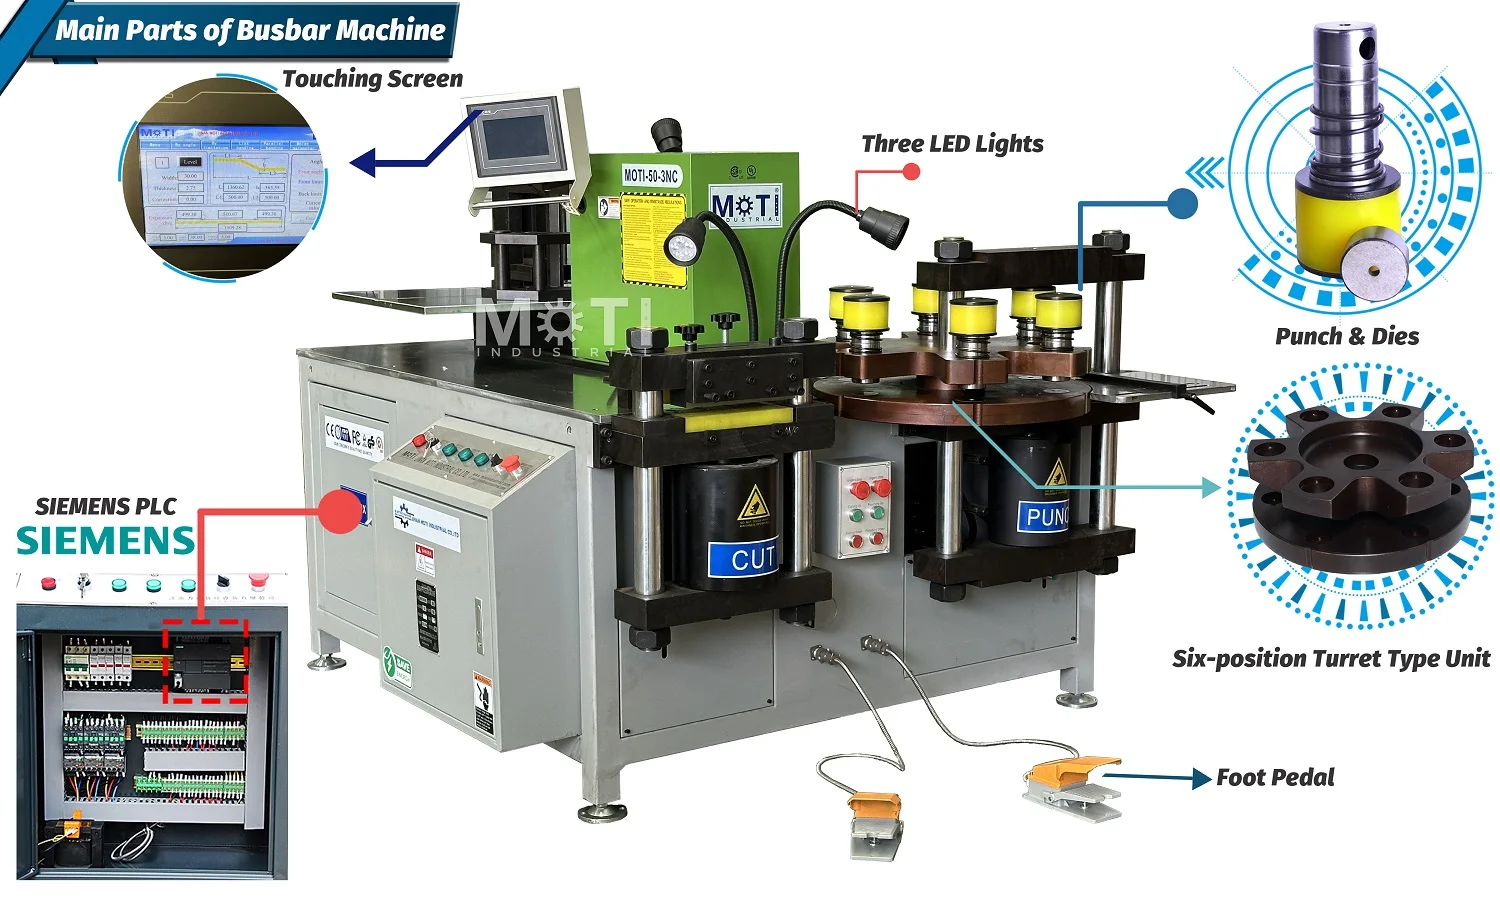
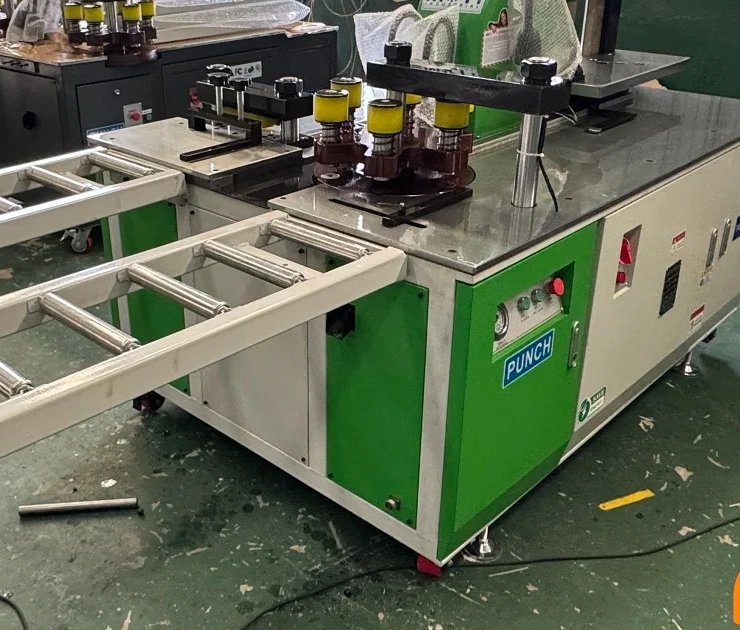
The double-column shearing unit, six-position punching turret and closed bending frame serve different stages of the job. This bending configuration uses Siemens control. Confirm the controller, die list and material supports for the version quoted for your order.

02 INSIDE THE PROCESS

See how the work gets done.

Equipment details, positioning and the workpiece requirements to discuss for this model.

01

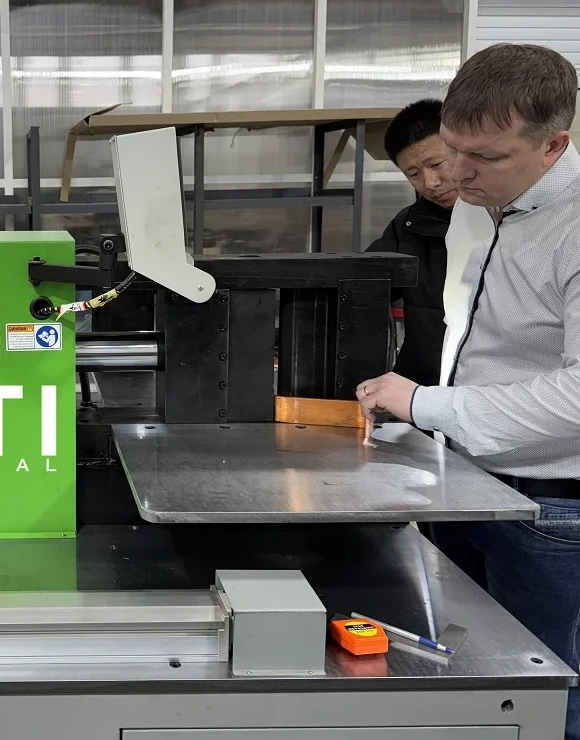
Cut to the next operation

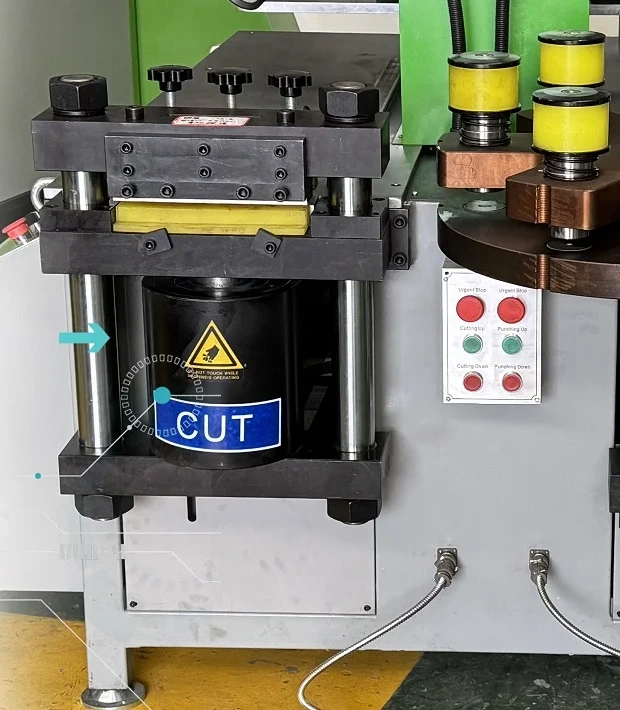
The hydraulic shearing station prepares busbar blanks for punching and bending in the 16 mm thickness class. Confirm working width for the selected machine configuration. Review the blade arrangement, length reference and offcut support with your actual bar, then check cut squareness and edge condition on a sample.

02

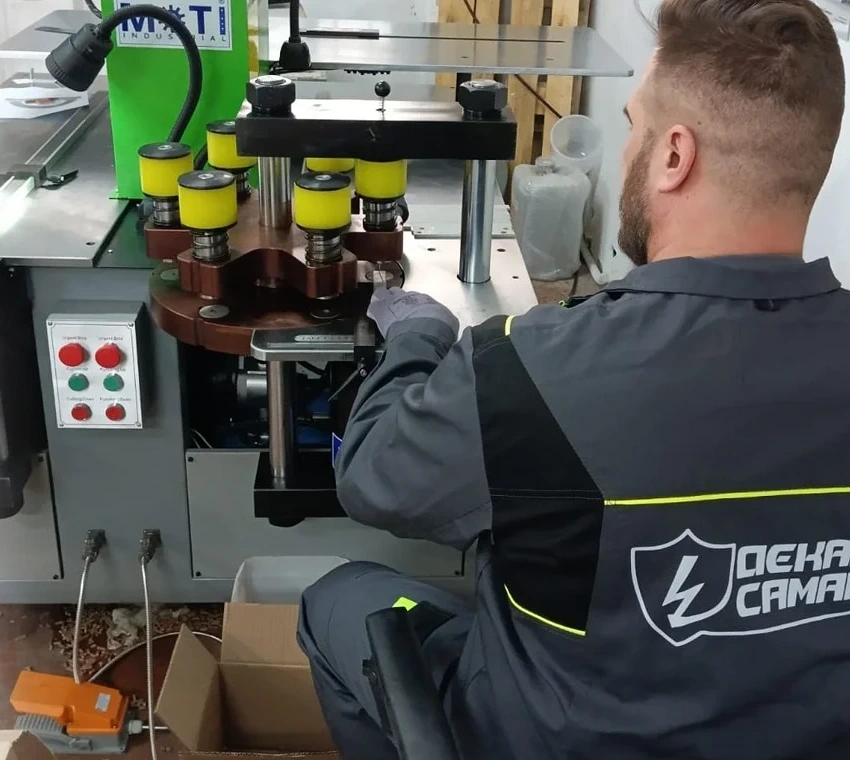
Keep common holes ready

The punching station uses a six-position turret so several commonly used dies can remain installed. The published hole-diameter range is 4.3–34 mm. Coordinate, positioning-pin and laser positioning methods are described for the series; specify the required arrangement in the quotation. Each die must be matched to the material and thickness—maximum bar capacity does not mean every small punch works at that thickness.

03

Form the connection

The CNC bending station uses a closed frame and digital angle control for repeat work. Select the tools around the bend direction, radius and complete finished shape, including short flanges and successive bends. Main-direction bending uses the 16 mm thickness class with width specified by configuration; the separate edge-bending limit is 12 mm thickness × 120 mm width. Twisting and special forms require a tooling review.

MOTI INDUSTRIAL · EQUIPMENT VIDEO

See the equipment in motion. Video from MOTI’s original product page and YouTube channel.

03 TOOLS & FINISHED PARTS

Tooling, configuration and options

Standard configuration: Specify the punch dies, cutting blades and matching bending tools for the quoted machine. The quotation identifies the hole sizes, quantities and tool interfaces.

Options: Connection-specific punch-and-bend tools and custom turret apertures are designed around your drawing, as in our HEMACK project. They are specified separately from the general tool package.

Punching dies

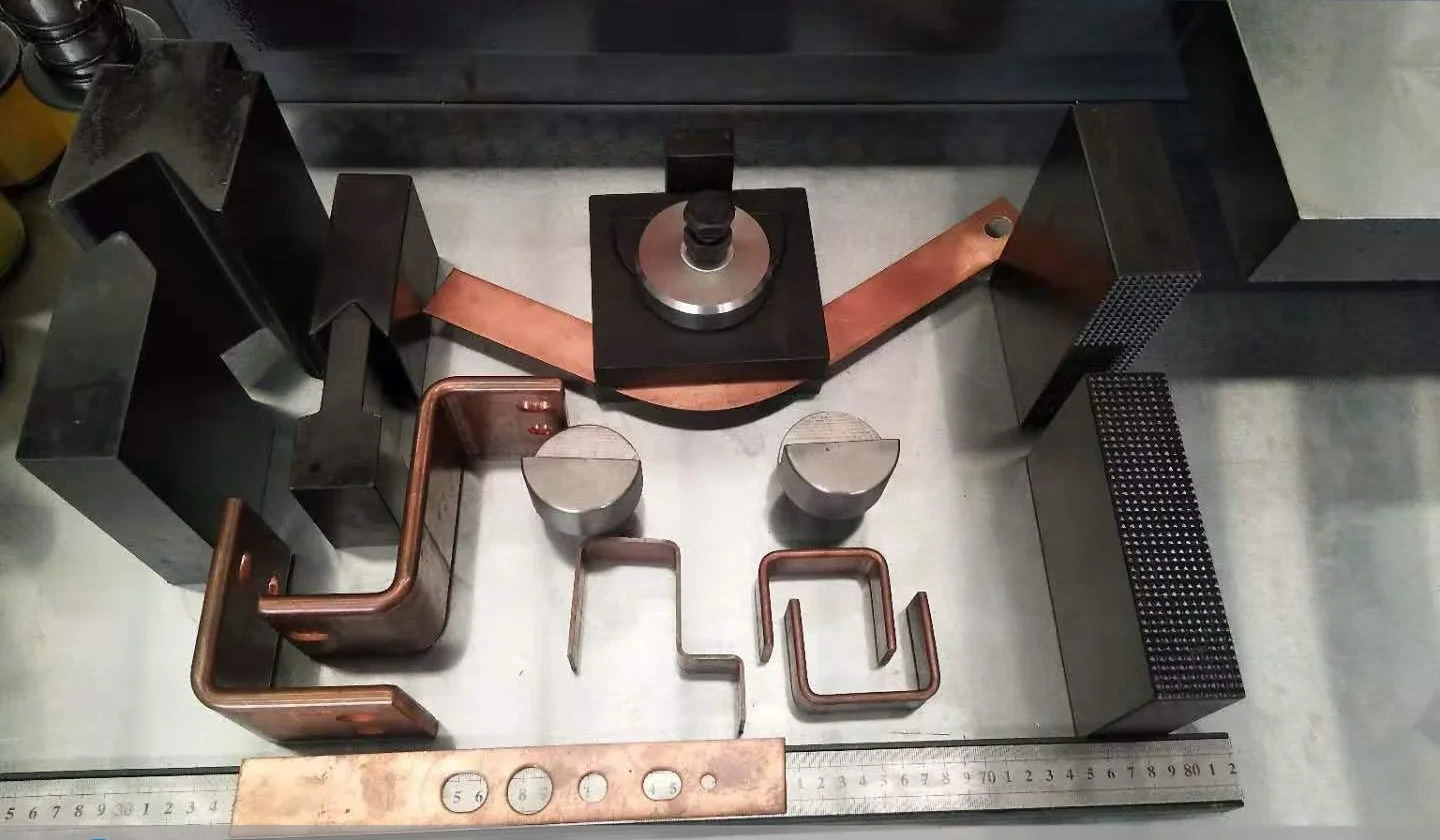
Specify each hole shape, size, quantity and required thickness. Include slot orientation and edge distance.

Bending tools

Define flat or edge bends, angle, radius, minimum flange and any U/Z sequence. The finished shape determines tool access.

Cutting blades

Confirm the blade set for the selected machine and material; include replacement blades if needed.

Special forming tools

Twisting, embossing or combined operations need a drawing and confirmation of the machine interface.

04 FROM SELECTION TO PRODUCTION

Review a complete working cycle.

01

Prepare the job

Identify the material, drawing revision and finished-part dimensions. Select the required punch and bending tools, set the cutting reference and provide support for the full bar length. Use the operating manual for setup and tool changes.

02

Make and check the first part

Check cut length, hole centers and the finished bend against the drawing. Keep the same datum through successive operations. For a new material batch or tool, check the first bend before applying the setting to the rest of the order.

03

Organize the repeat work

The three independent hydraulic workstations allow cutting, punching and bending to be organized in parallel. Plan the operators’ working areas, part transfer and material supports. Actual output depends on the whole job, including loading, positioning and inspection.

05 MOTI-50-3NC · QUESTIONS

Before you choose.

The 50-3NC covers the 16 mm thickness class, with working width specified by configuration. Compare your part with the punching diameter, edge-bending limit, motor power and handling requirements. Edge bending has a separate 12 mm thickness × 120 mm width limit. The drawing and quoted machine configuration determine the suitable choice.
No. The standard machine requires workpiece handling and positioning at the workstations. CNC bending control and independent hydraulic systems do not make it an automatic production line. For servo-assisted positioning at cutting, punching and bending, compare the 50-3NC PRO.

The standard series distinguishes a published bending accuracy of ±1° from repeat bending accuracy of ±0.3°. These are different measures. Your trial should state the material, tooling, angle and measuring method, and check the completed part.

Yes. Send a dimensioned drawing with material, thickness, bend radius and angle, holes and assembly references. We can discuss the tool design and whether the existing turret or fixture needs a custom interface.

06 COMPARE OPTIONS

Find the right level of capability.

Servo 3-in-1

Four servo positioning axes for repeated work.

16 × 250 mm

Thickness × width · operation limits apply

MOTI-30-3NC MAX workstation detail

Wide-format 3-in-1

More width in the 12 mm thickness class.

12 × 200 mm

Thickness × width · operation limits apply

Heavy-duty 3-in-1

For thicker and wider copper busbars.

20 × 300 mm

Thickness × width · operation limits apply

Tell us about the busbars you make.

Share your material, maximum thickness and width, and the cutting, punching or bending work you need. A drawing or a sample requirement helps us discuss the right machine and tooling.

We use your details to respond to your machine enquiry. For drawings, use the email or WhatsApp links below.

Have a drawing? Attach your PDF, CAD file or clear part photo in email or WhatsApp. Include material, thickness, width and quantity.

Back to top