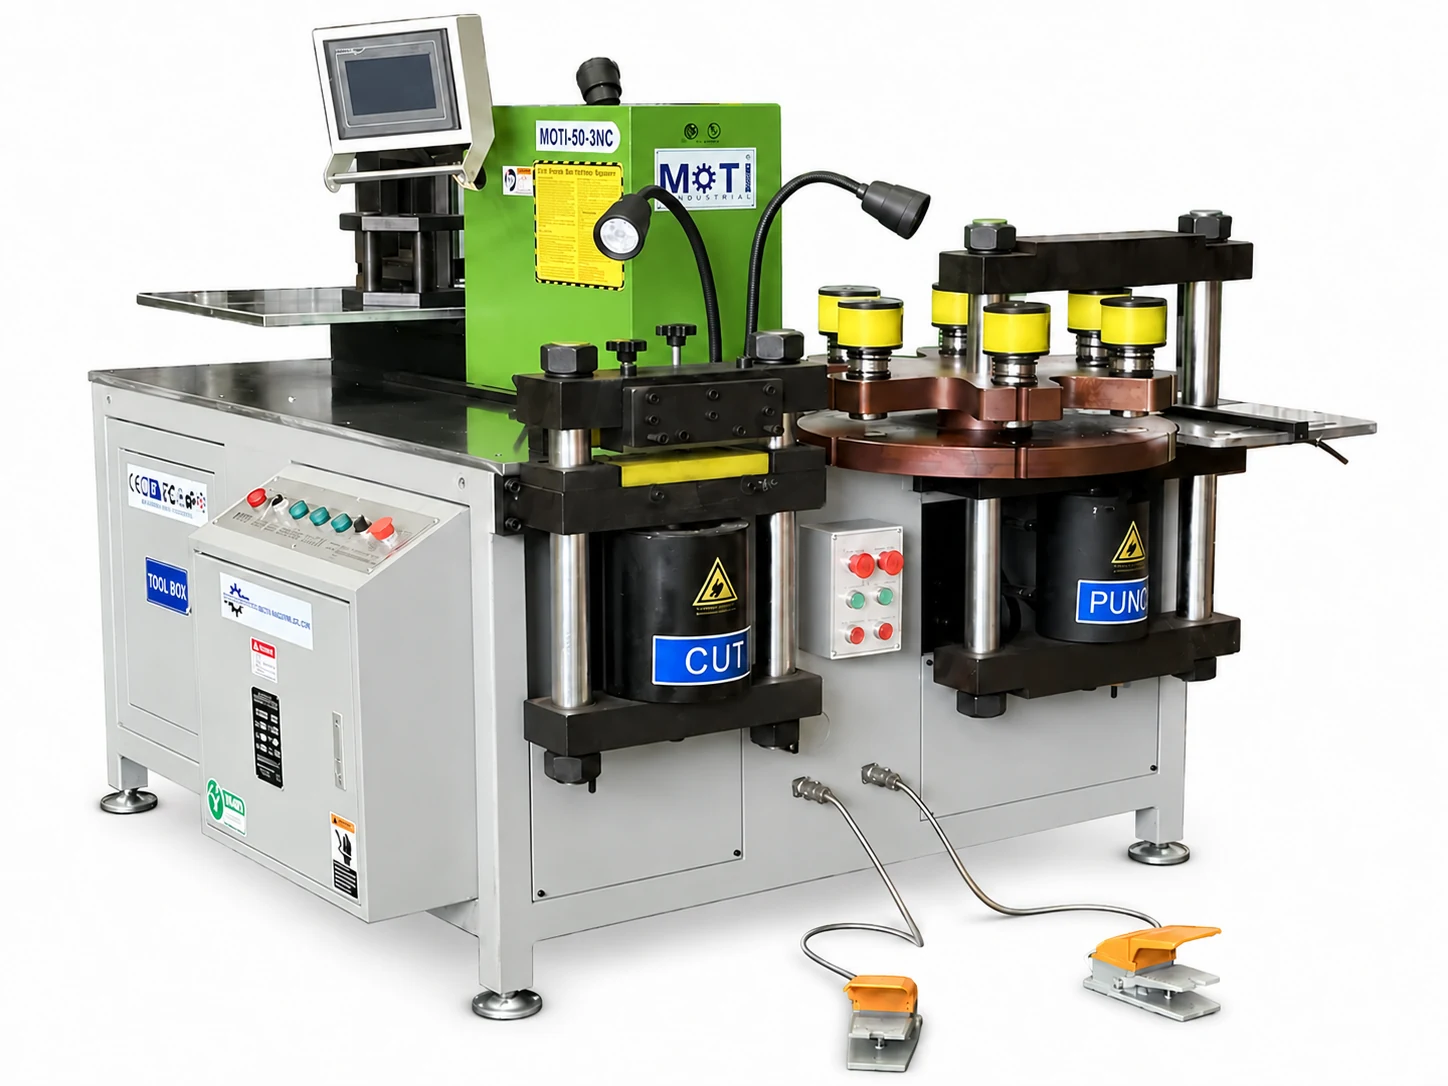
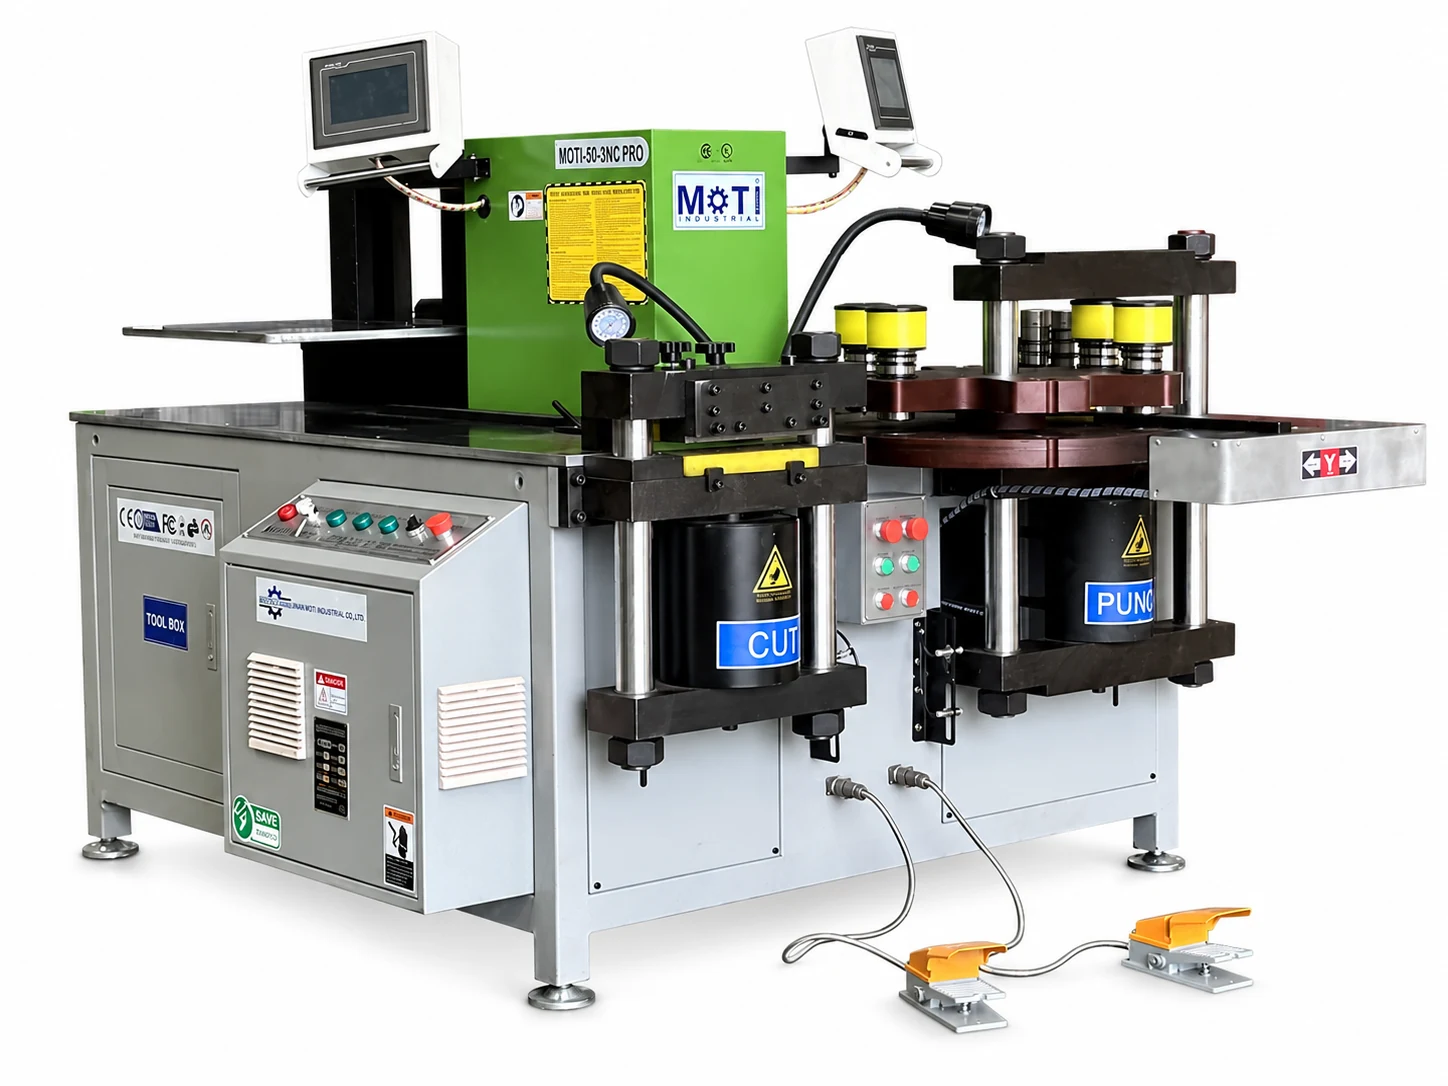
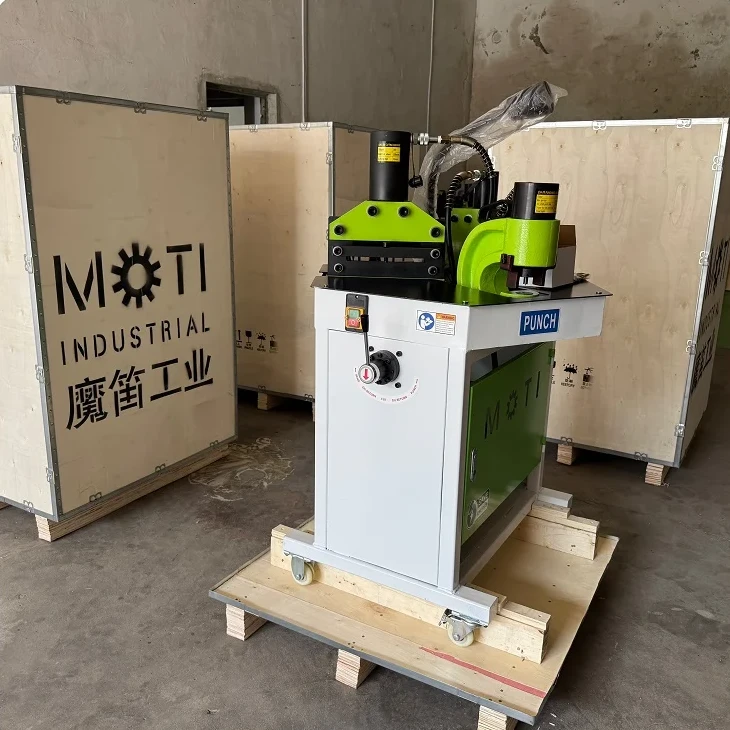
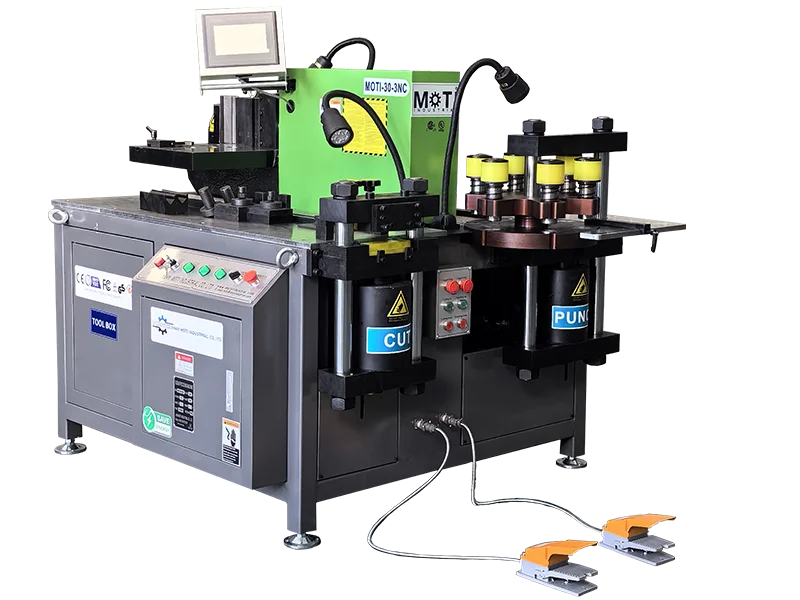
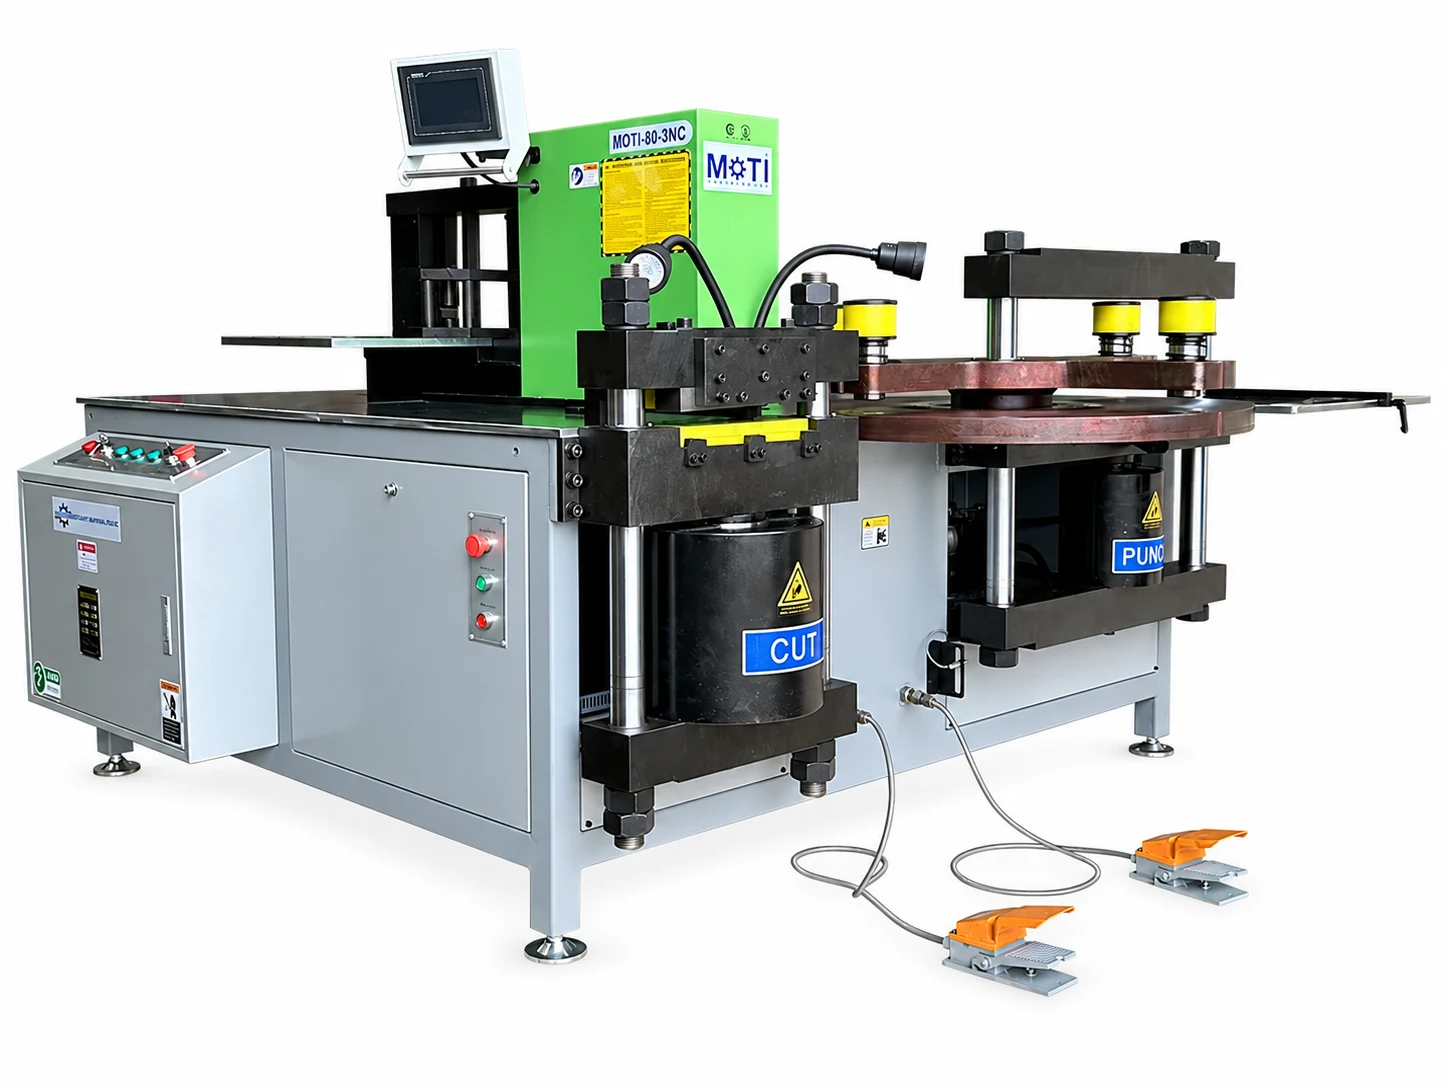
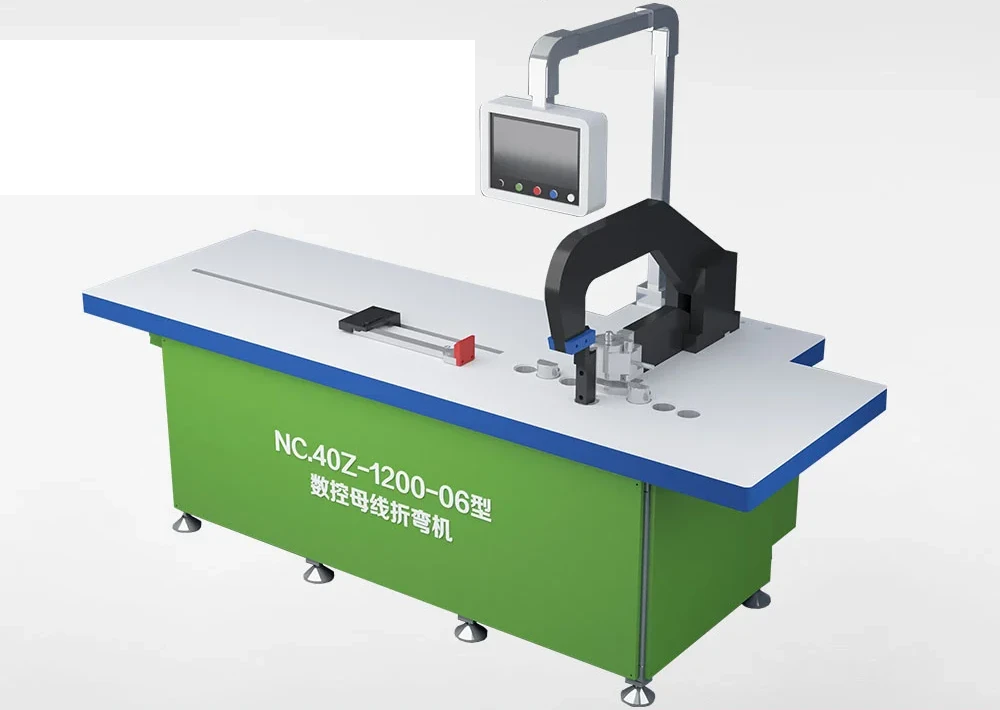
Standard 3-in-1

Cut, punch and bend. Standard, wider MAX and heavy-duty models.

Servo 3-in-1

Four positioning axes. Operators move parts between stations.

Portable Hydraulic

Separate cutting, punching and bending tools with hydraulic power.

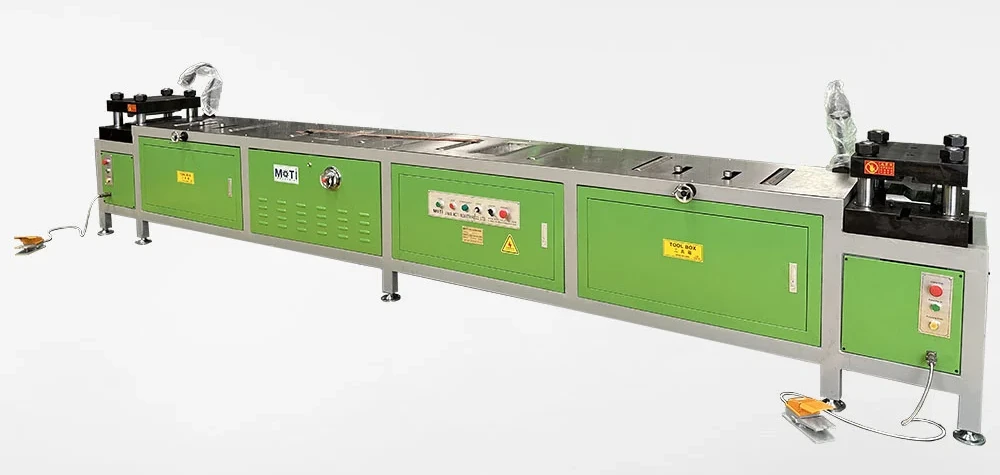
Dedicated Bending

CNC bending centers or double-head busduct connection bending.

CUSTOM TOOLING & PROCESS CONFIGURATIONS

Custom busbar punching dies and bending tools

Special hole shapes, short connections and repeated punching patterns need more than a capacity figure. Share the finished part and let the process define the tooling discussion.

Customize the tool, station or support

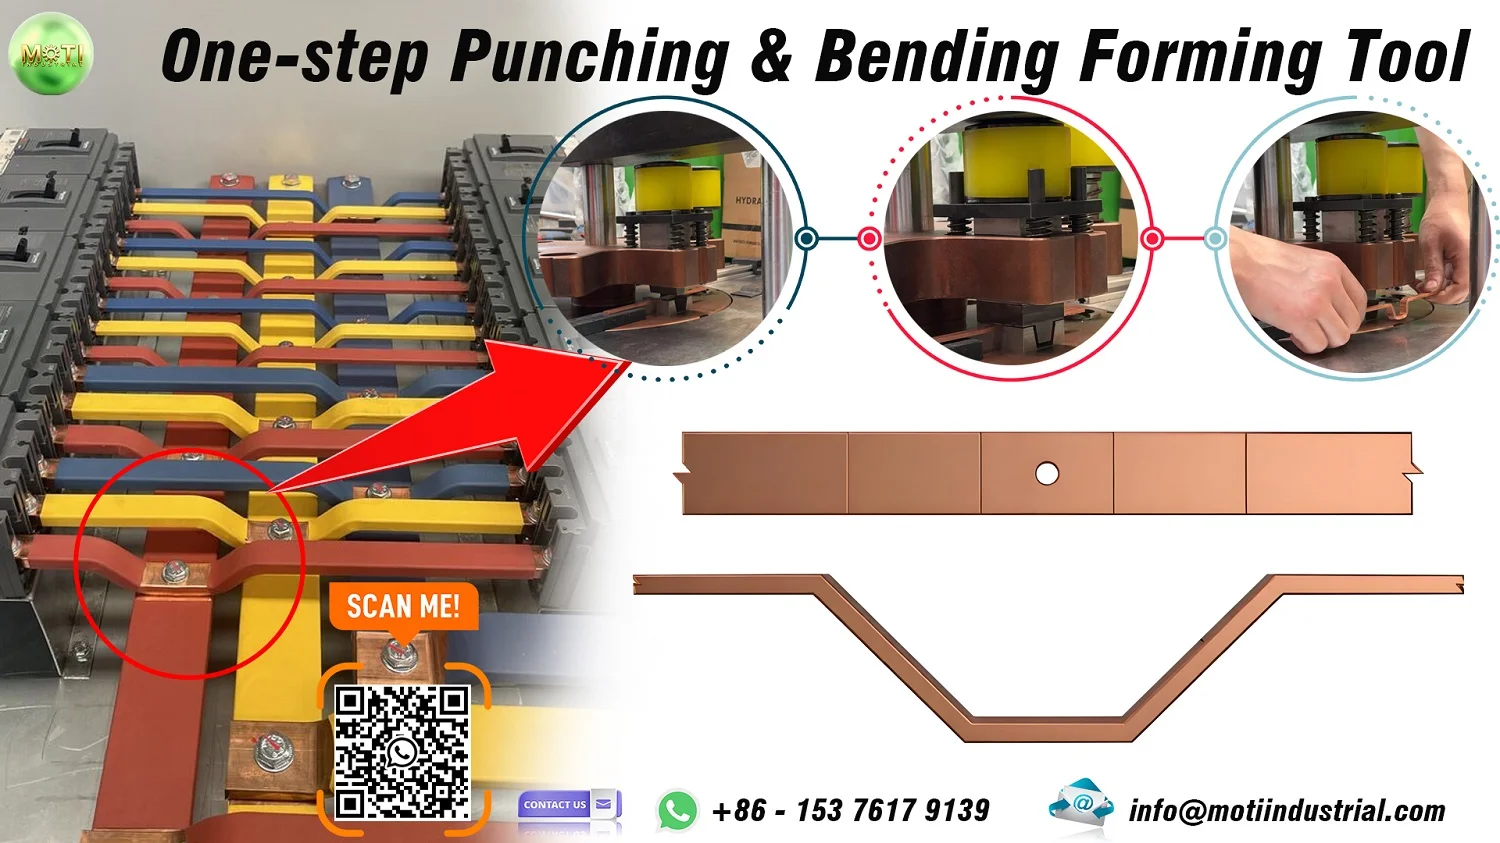
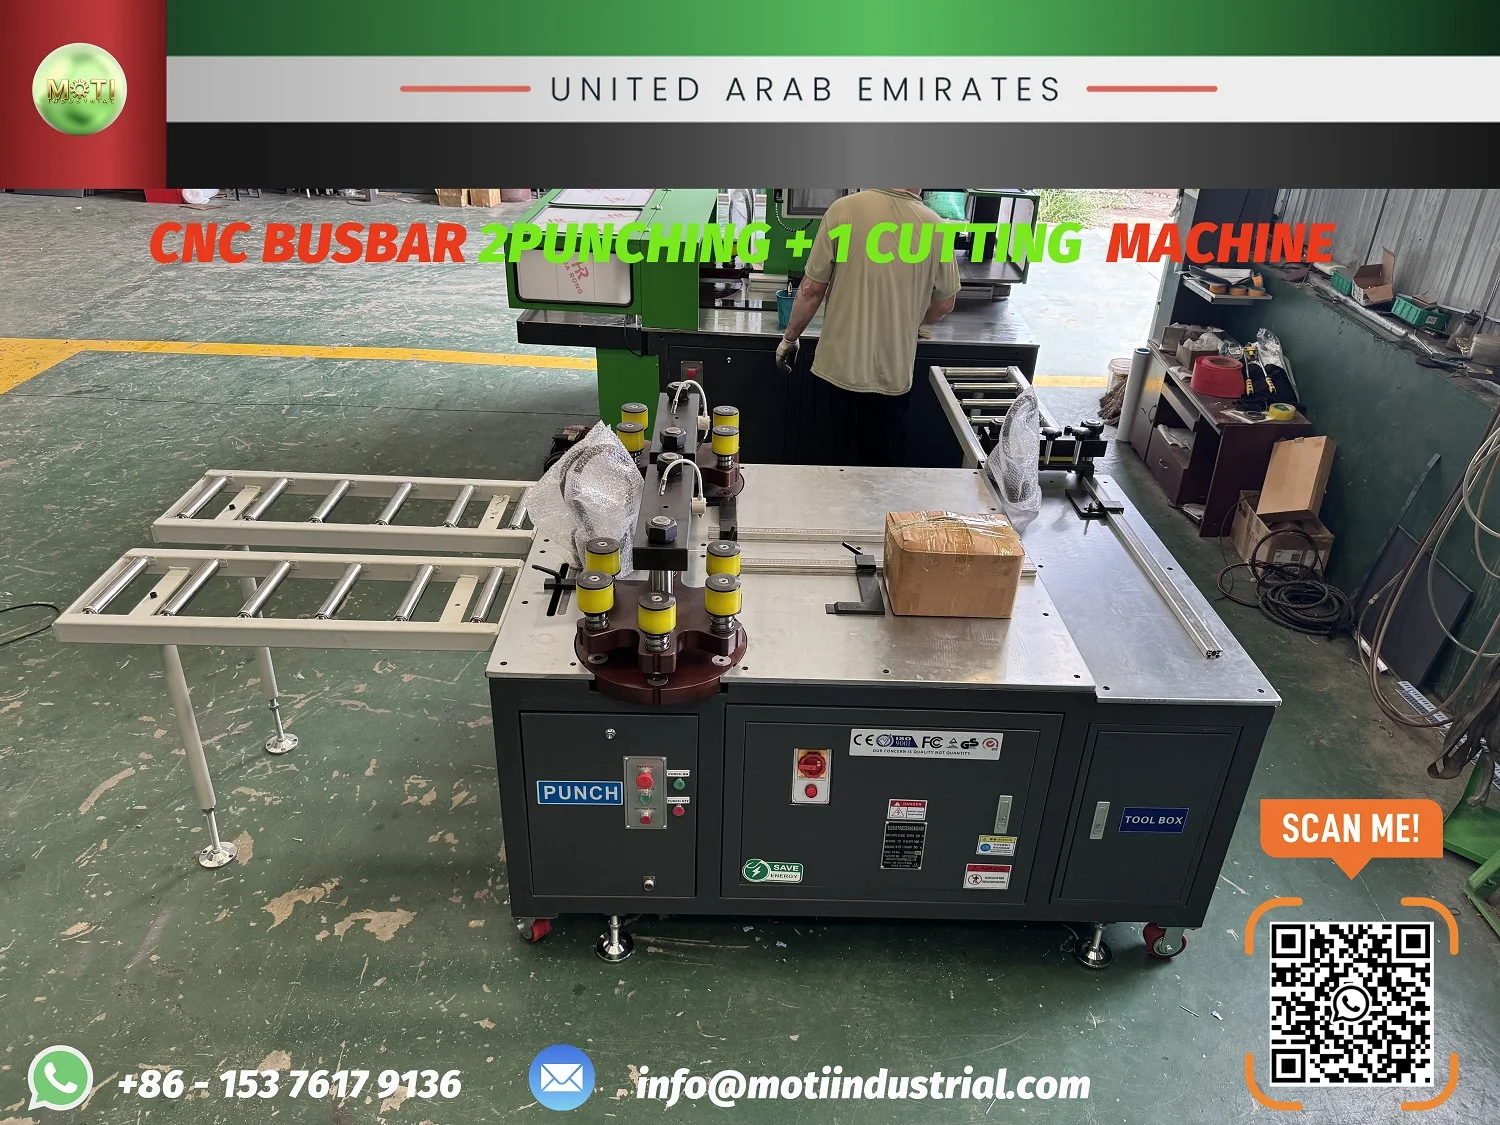
The HEMACK project combines punching and bending in a drawing-specific tool. A separate UAE delivery uses two punching stations and one cutting station, with detachable leveling supports. Discuss the actual bottleneck, hole geometry and handling route before choosing a custom configuration.

One-step punching and bending tooling illustrated in the HEMACK project article.

Custom holes and forming tools

Include the hole profile, tolerances, material thickness, edge distances and machine interface. MOTI’s HEMACK project describes discussions around dedicated connection tooling and single-operation punching and bending tools.

A different mix of workstations

In an UAE project, MOTI documented a manually controlled configuration with two punching units and one cutting unit for 12 × 160 mm copper bars. Each punching unit used a six-die turret. This is an example of adapting the workstation mix to a process.

Define a useful trial

Agree on the drawing revision, material, tool set, inspection points and acceptance criteria. Compare loading, positioning, changing tools and checking the part as well as the cutting or punching stroke.

The interface matters as much as the shape

The HEMACK combined tool places a bending die below the punch and requires a custom-machined turret opening. A drawing-led tool proposal therefore needs the machine model and interface dimensions as well as the desired finished bar.

Make hole changes easier to evaluate

List the hole patterns you repeat and the tools used for each. A turret keeps several dies available; servo positioning assists the reference coordinates; a second punching workstation changes how work can be divided. Choose between them using your actual job mix.

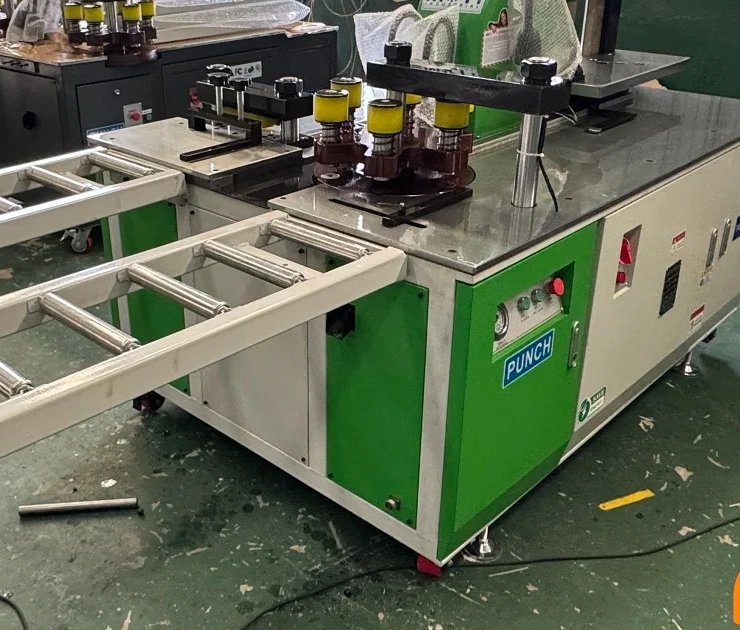
Custom two-punching, one-cutting machine prepared for the UAE project.

Record the sample and tool together

Keep the drawing revision, material, tool identification and inspected dimensions with the approved sample. This creates a useful reference for repeat orders and future tool replacement.

IN THIS GUIDE

Have a similar part?

Send your drawing, material size and production requirements. Include the holes and bends you need to make.
01 RELATED EQUIPMENT

Explore the machine options.

3-in-1 workstation

A wider working range for panel production.

16 mm thickness class

Thickness × width · operation limits apply

Servo 3-in-1

Four servo positioning axes for repeated work.

16 × 250 mm

Thickness × width · operation limits apply

Double-head bending

For busduct connection bars and end forming.

3 × 30 to 6 × 200 mm

Thickness × width · operation limits apply

Tell us about the busbars you make.

Share your material, maximum thickness and width, and the cutting, punching or bending work you need. A drawing or a sample requirement helps us discuss the right machine and tooling.

We use your details to respond to your machine enquiry. For drawings, use the email or WhatsApp links below.

Have a drawing? Attach your PDF, CAD file or clear part photo in email or WhatsApp. Include material, thickness, width and quantity.

Back to top